SHOP SOLUTIONS
KEEP IT CLEAN

KEEP IT CLEAN

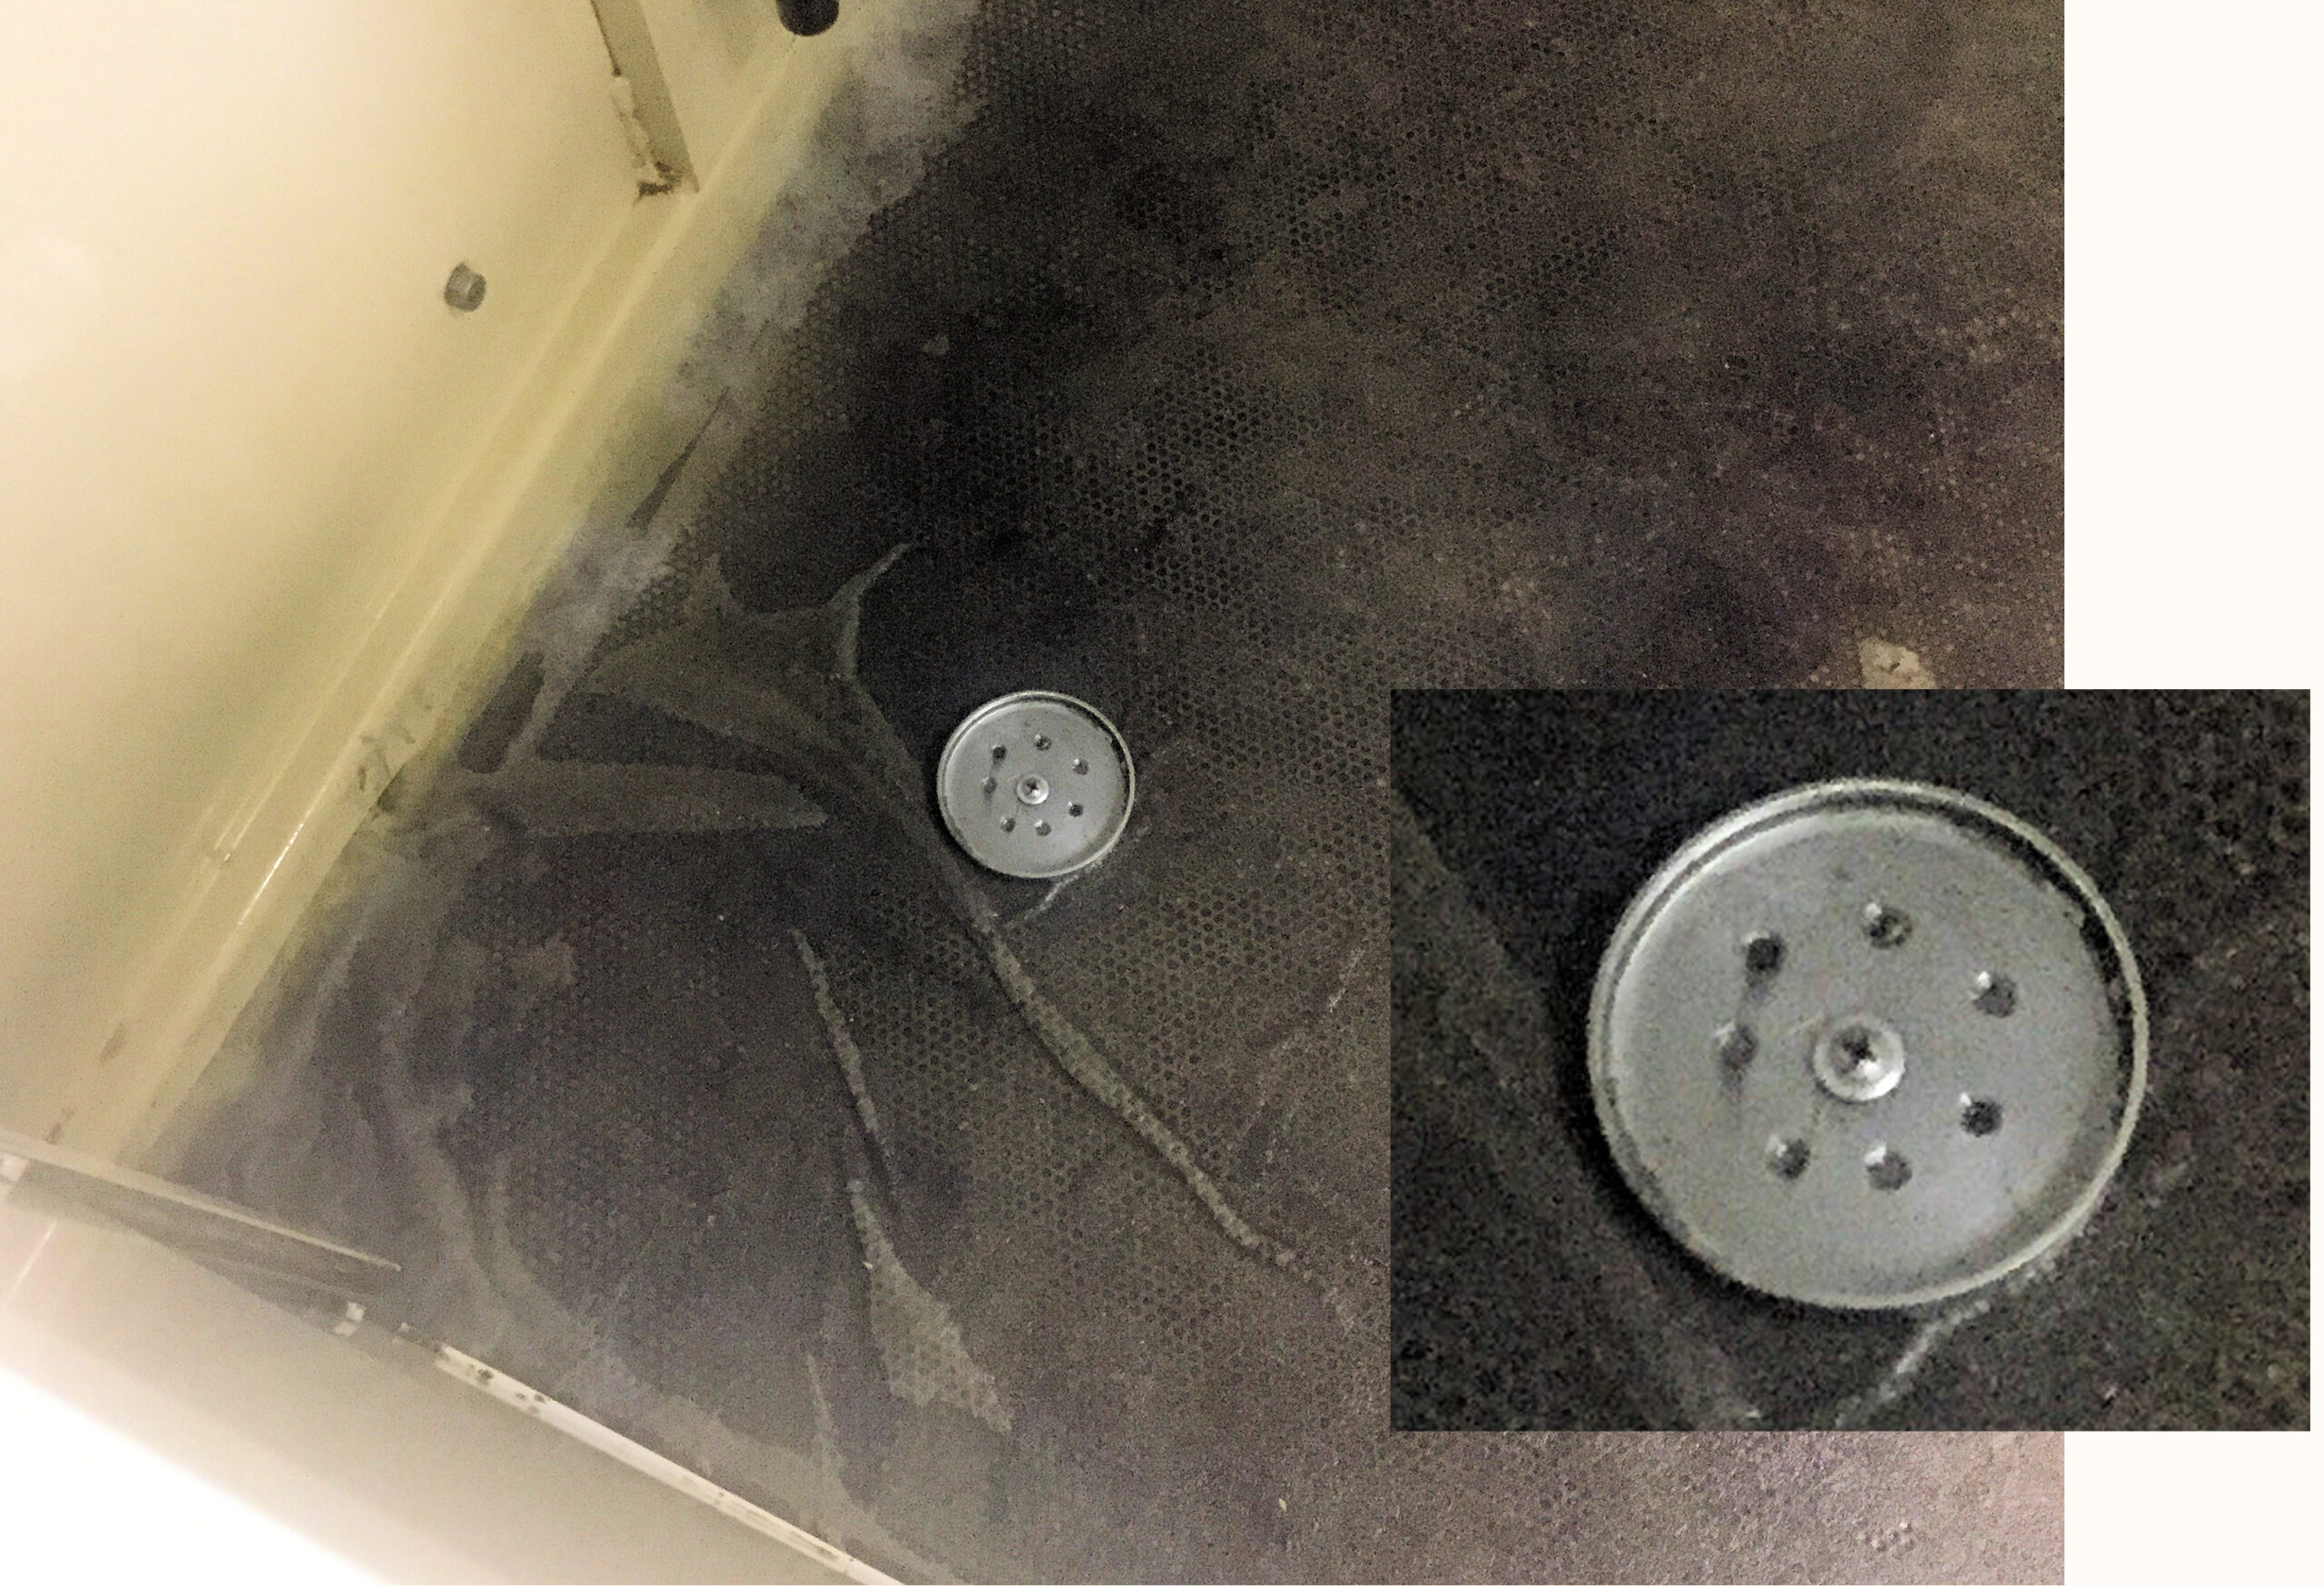
KEEP IT CLEAN On the line honing machine, the mandrel rest and tank sides can end up becoming a real mess, especially after the job while the mandrel drains off. I took a large cup freeze plug and drilled some drain holes in it. I screwed this to the metal screen...
read more
SHIM IT

SHIM IT

SHIM IT We shim many different components to get square or level before we machine. Don't forget the rod and cap when cutting for resizing. Shim to get the parting surface to cut as the factory did whether it's 90 degrees to the sides or not, and your rods will turn...

read more
THRUST WATCH

THRUST WATCH

THRUST WATCH As engine builders we always make sure the crankshaft thrust is proper before assembling the rest of the engine. I believe we should also be measuring it again when it is in the vehicle because there are so many possible flywheel/clutch, torque converter...

read more
QUICK T-NUTS

QUICK T-NUTS

QUICK T-NUTS Start with a carriage bolt with a head diameter 1/4" larger than the bottom of the T-slot. Be sure the bolt's square shank fits easily into the T-slot. Chuck the bolt in the lathe, drill and tap thru the head to a depth just beyond the end of the square...

read more
GET IT STRAIGHT

GET IT STRAIGHT

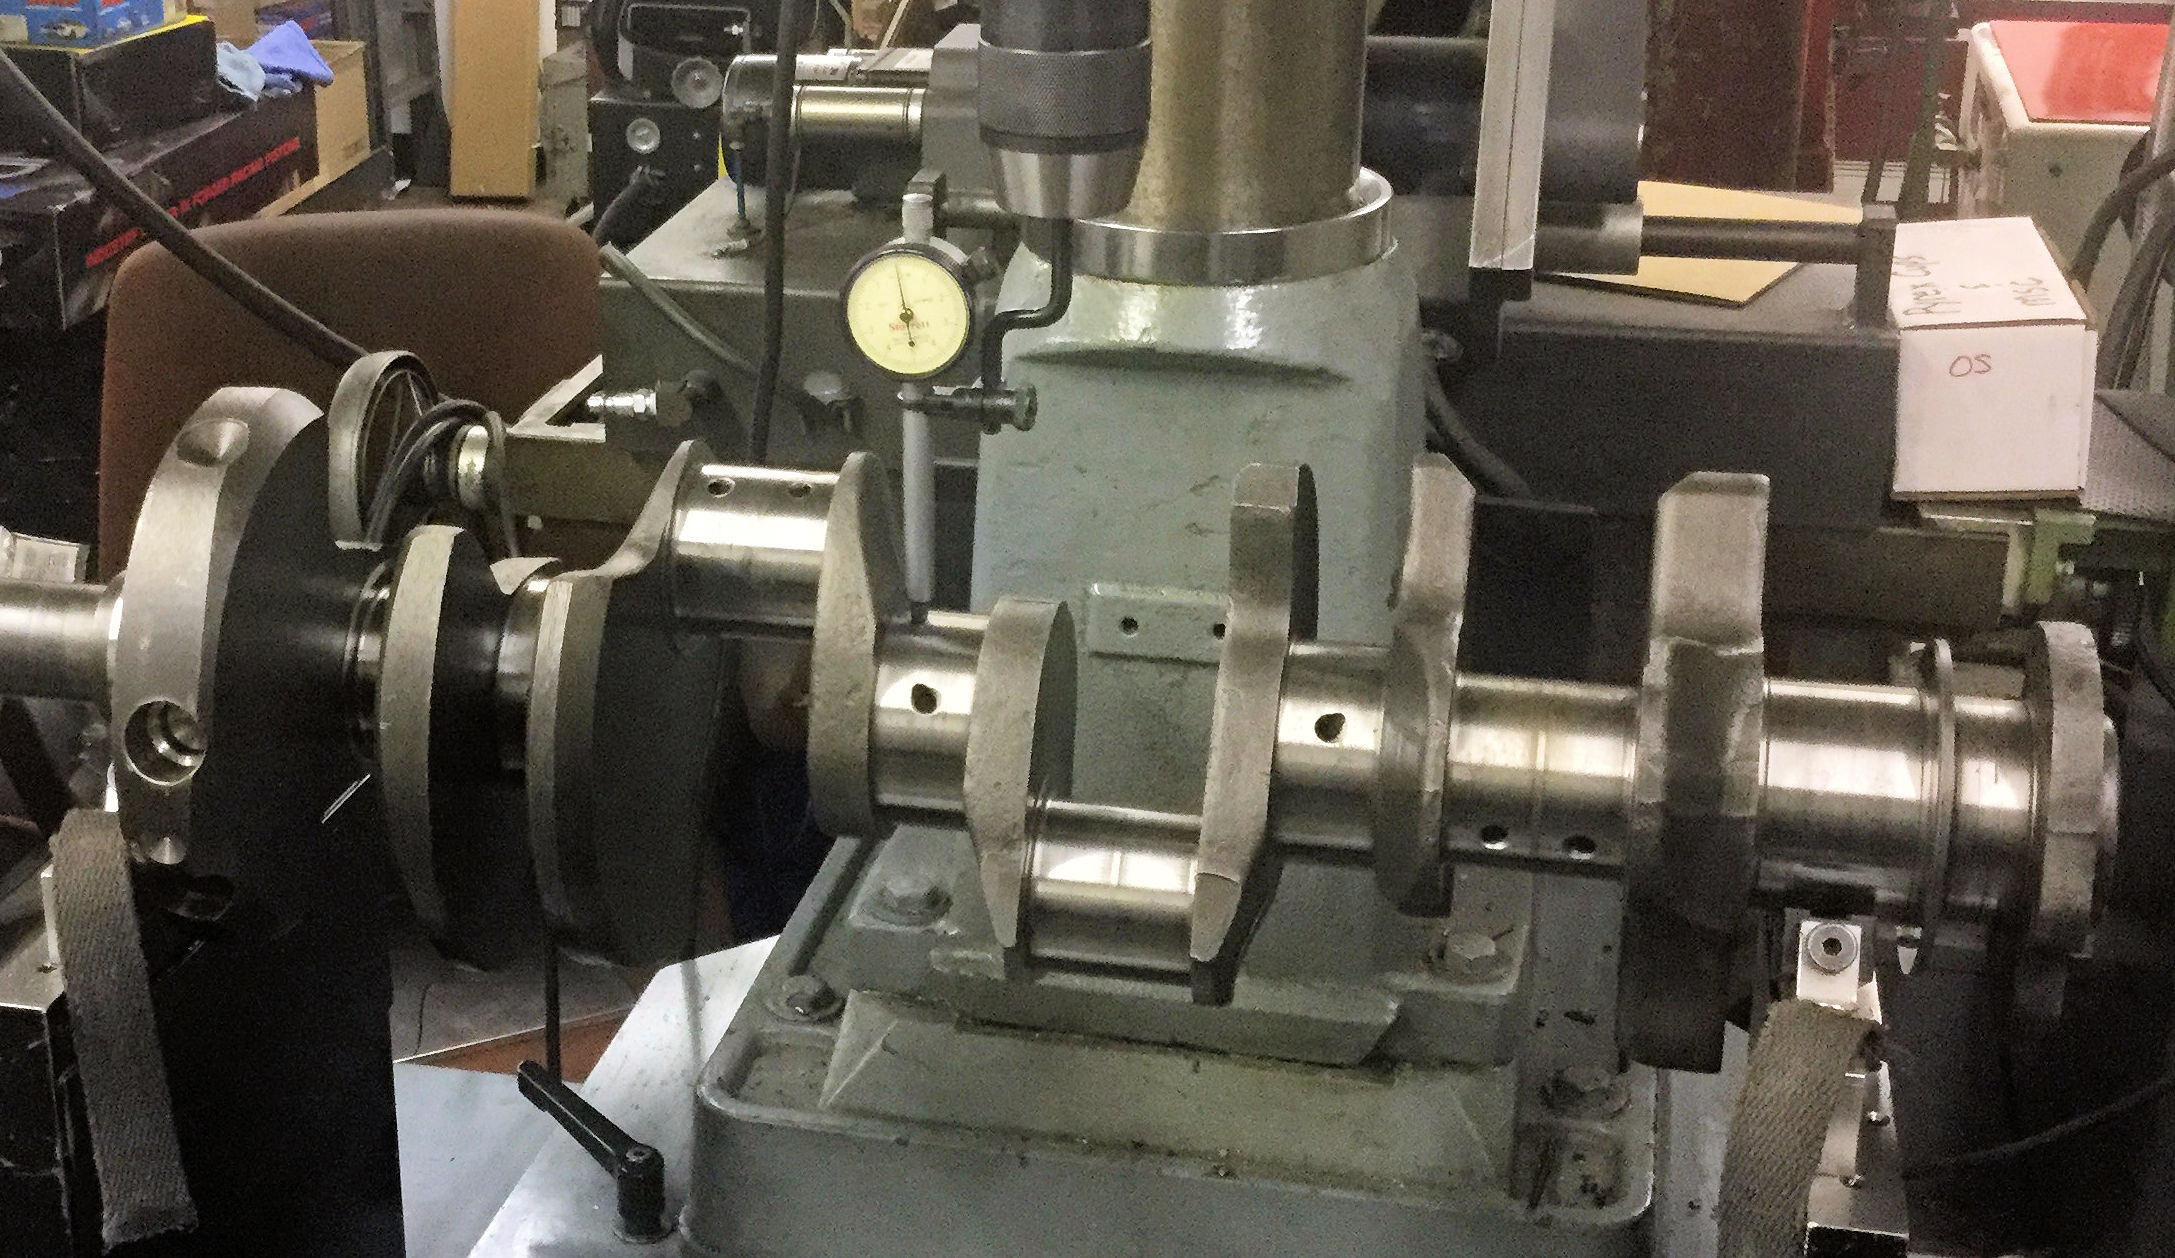
GET IT STRAIGHT When balancing crankshafts, I feel I is imperative that the crank straightness be checked and corrected for before any balance work is done to ensure accuracy. I have an offset indicator that I’ve come up with that mounts right in the mill drill on the...

read more
BLUE BE GONE

BLUE BE GONE

BLUE BE GONE Metal parts that are exposed to too much heat will turn a shade of Blue. I found that brushing white vinegar on the eye of the connecting rod, after heating to install pistons, removes the Blue. Put vinegar in a plastic container for dipping small parts,...

read more