SHOP SOLUTIONS
INDICATOR ADAPTER

INDICATOR ADAPTER

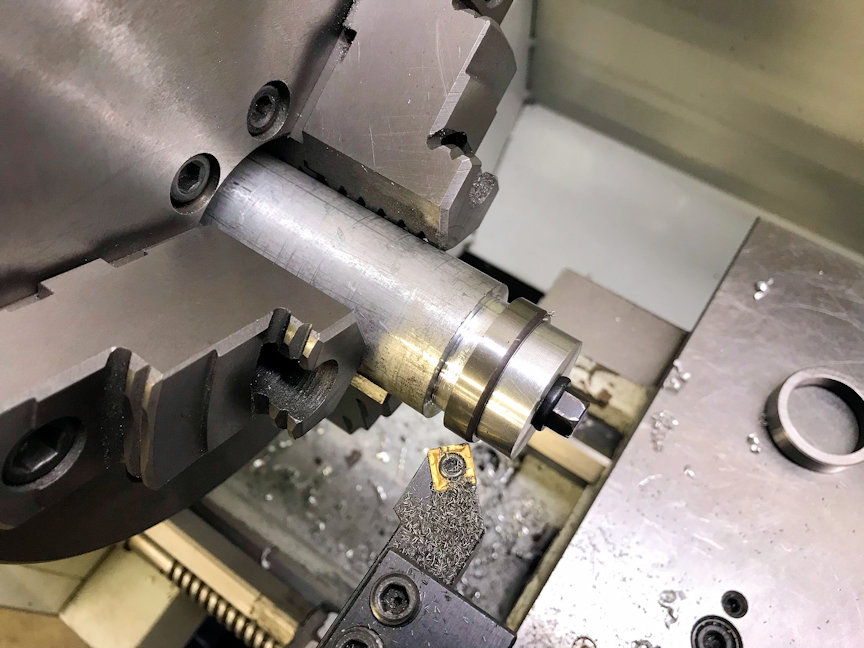
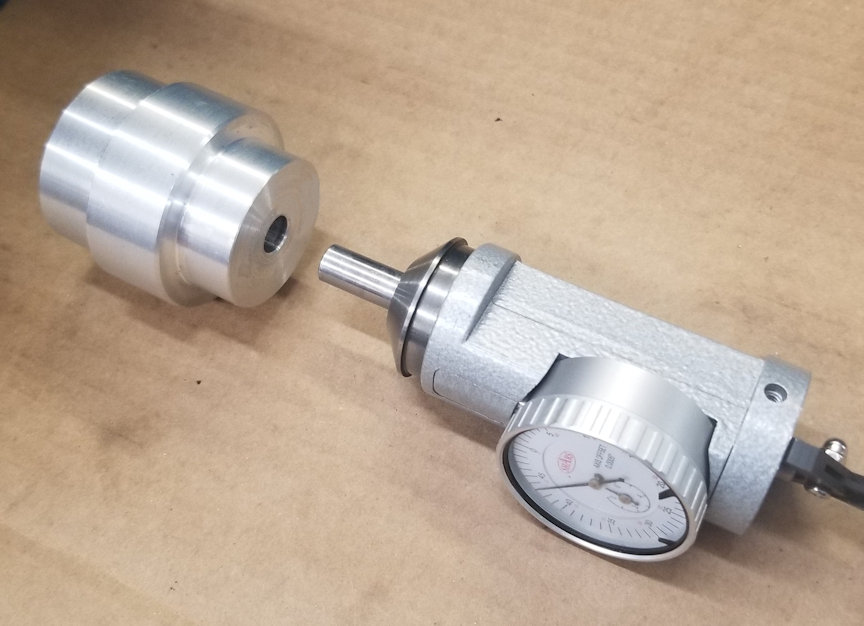
INDICATOR ADAPTER Most Co-Ax indicators have a 3/8" or 1/2" diameter stem. Instead of wasting time closing the lathe chuck to hold the indicator and then more time opening it back up to hold a larger diameter work piece, make a simple stepped adapter with a precision...
read more
SEAT SPUD

SEAT SPUD

SEAT SPUD For machining custom valve seats, in addition to the expansion arbor, I have a simple aluminum spud and lock. I can quick machine it down for whatever seat I need. It started out as a 1-foot-long piece of round stock, and I just keep drilling and tapping as...

read more
POWER ADJUSTMENTS

POWER ADJUSTMENTS

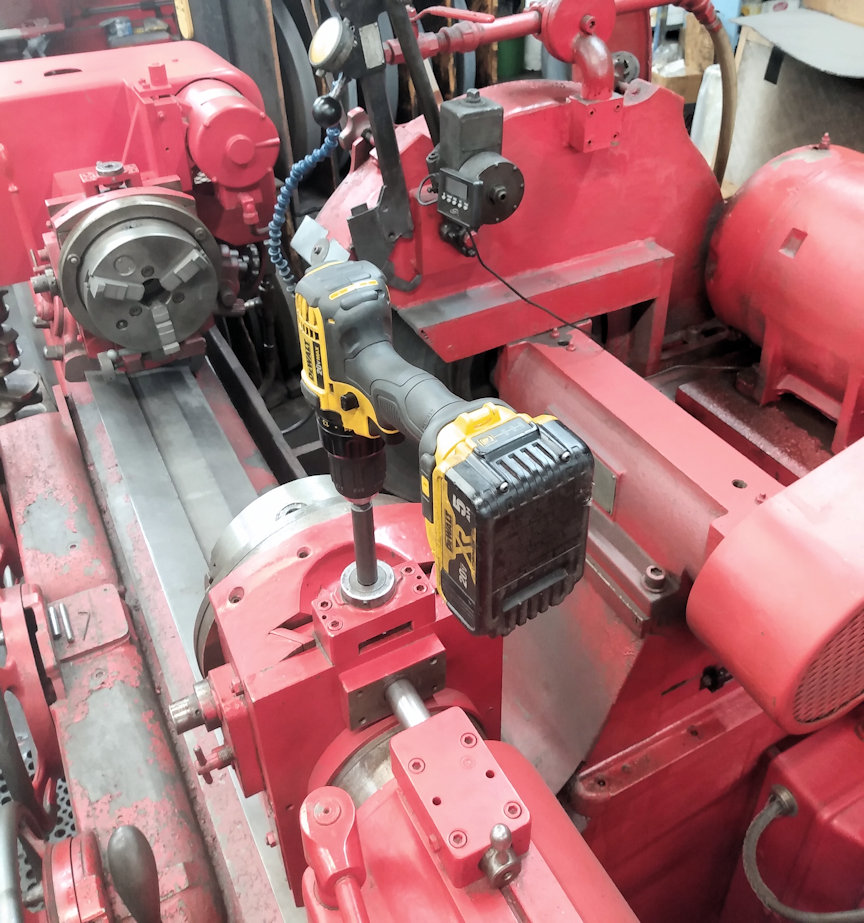
POWER ADJUSTMENTS To save time, we use a half inch cordless drill to power our stroke and counterweight adjustments on our crankshaft grinder machines. Adney Brown Performance Crankshaft Ferndale, MI DECEMBER, 2021

read more
SET UP BLOCKS

SET UP BLOCKS

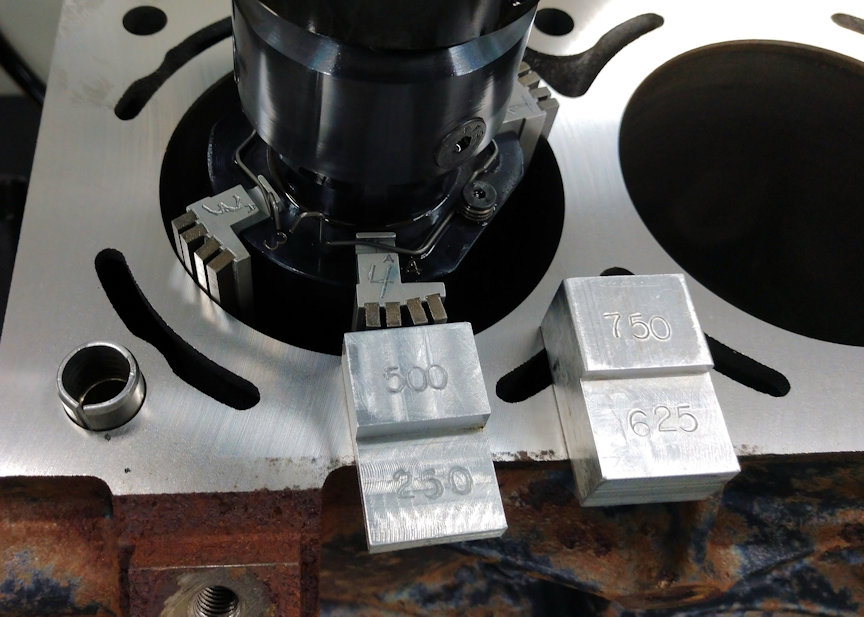
SET UP BLOCKS Keep your tape measure in the toolbox when doing set ups that you repeat time and time again. Make some gauge blocks or fixtures, whatever it takes to save time setting up your machines. Randy Torvinen Torvinen's Machine Menahga, MN DECEMBER, 2021

read more
BLOCK SQUARED

BLOCK SQUARED

BLOCK SQUARED For those using the common block deck indexing fixture, here’s an easy way to check accuracy of the front plate. When you finish squaring up a block. Flip the plate backwards and check the deck across the surface to the plate again. It should read the...

read more
GET YOUR BEARINGS

GET YOUR BEARINGS

GET YOUR BEARINGS When baking and shot peening cylinder blocks, I leave the main bearing shells and the cam bearings in the block to protect surfaces and maintain concentricity. Anthony Rotella Anthony’s Marine & Service St Petersburg, FL NOVEMBER, 2021

read more