BROWSE BY CATEGORY
BROWSE ALL SHOP SOLUTIONS
COVER ALIGNMENT
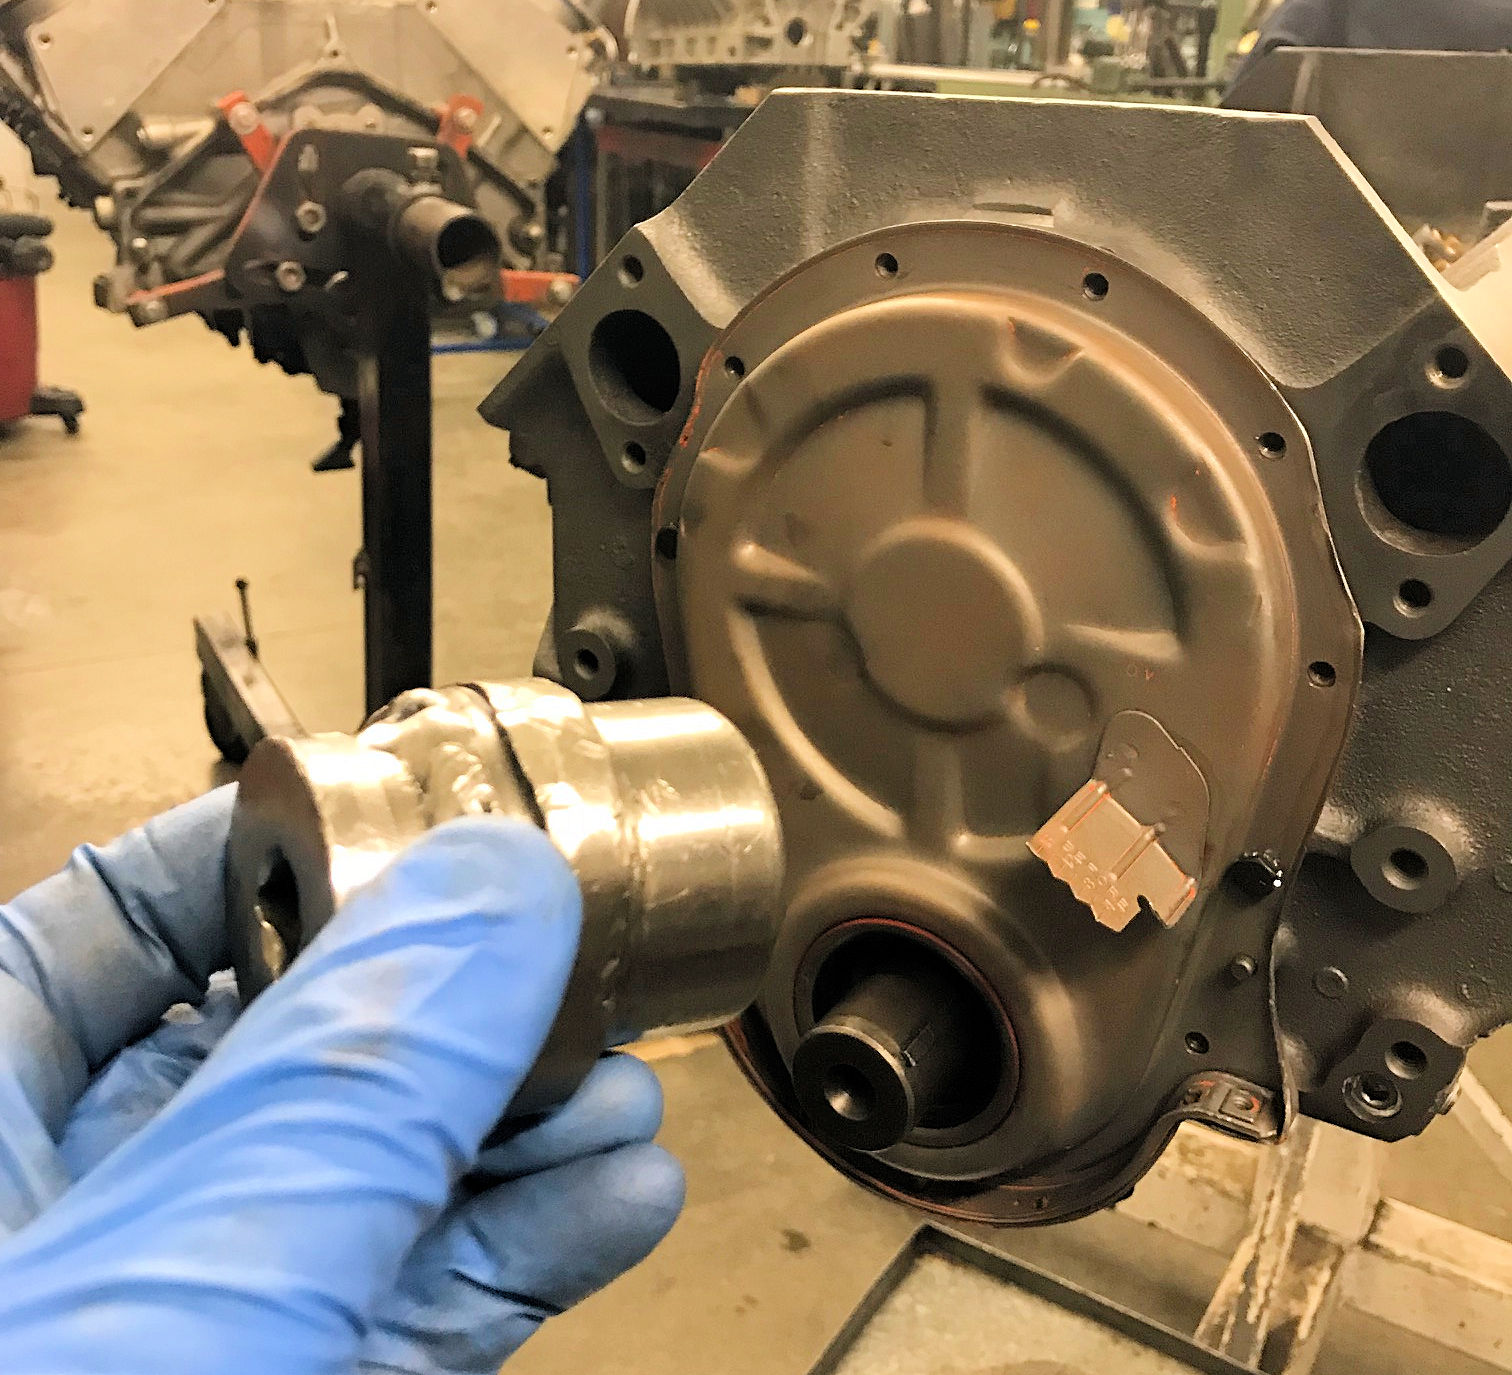
COVER ALIGNMENT On many engines with timing covers that are located by dowel pins, there can me misalignment problems that may result in a leak. To eliminate this is, I drill the dowel pin locator holes in the cover one or two sizes oversize. Then I set it up in place...
NUMBER YOUR STONES
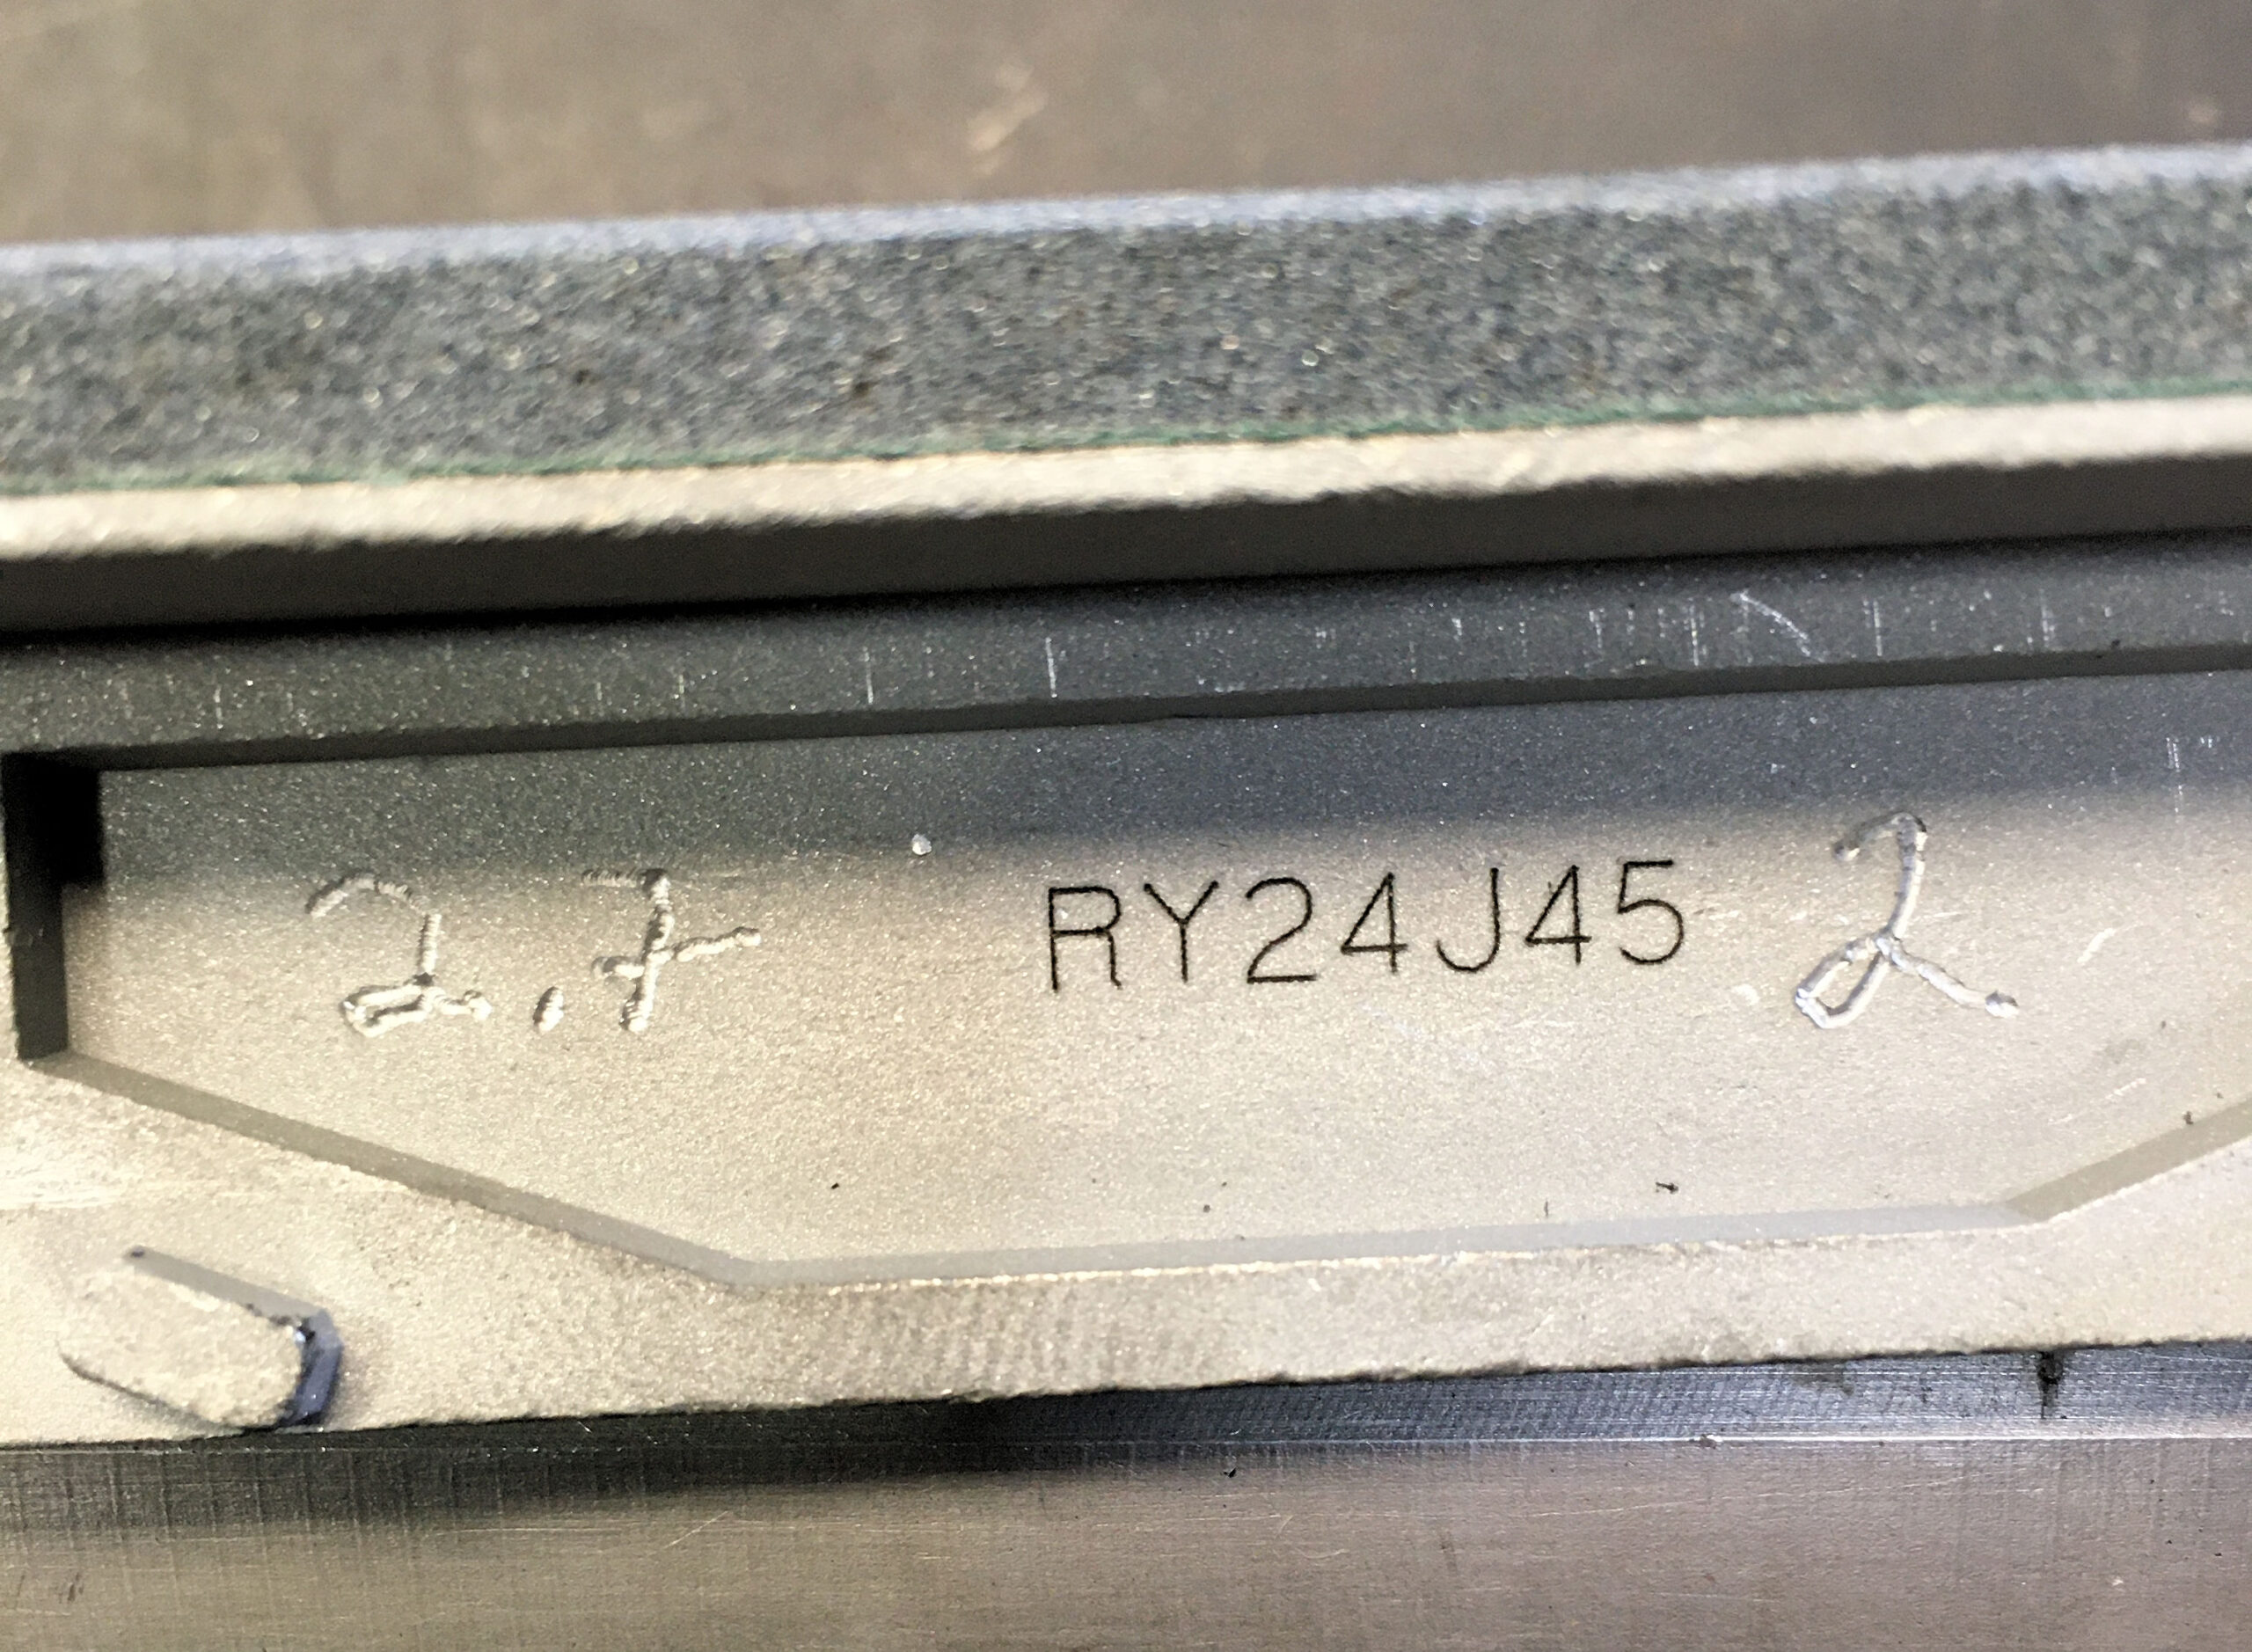
NUMBER YOUR STONES When changing stones on your line hone from cast iron blocks to aluminum blocks with billet caps, I take an engraving tool and engrave a #1 on my mandrels to mark where to start and engraved the stone position and mandrel size into each stone. It...
ANOTHER ARBOR
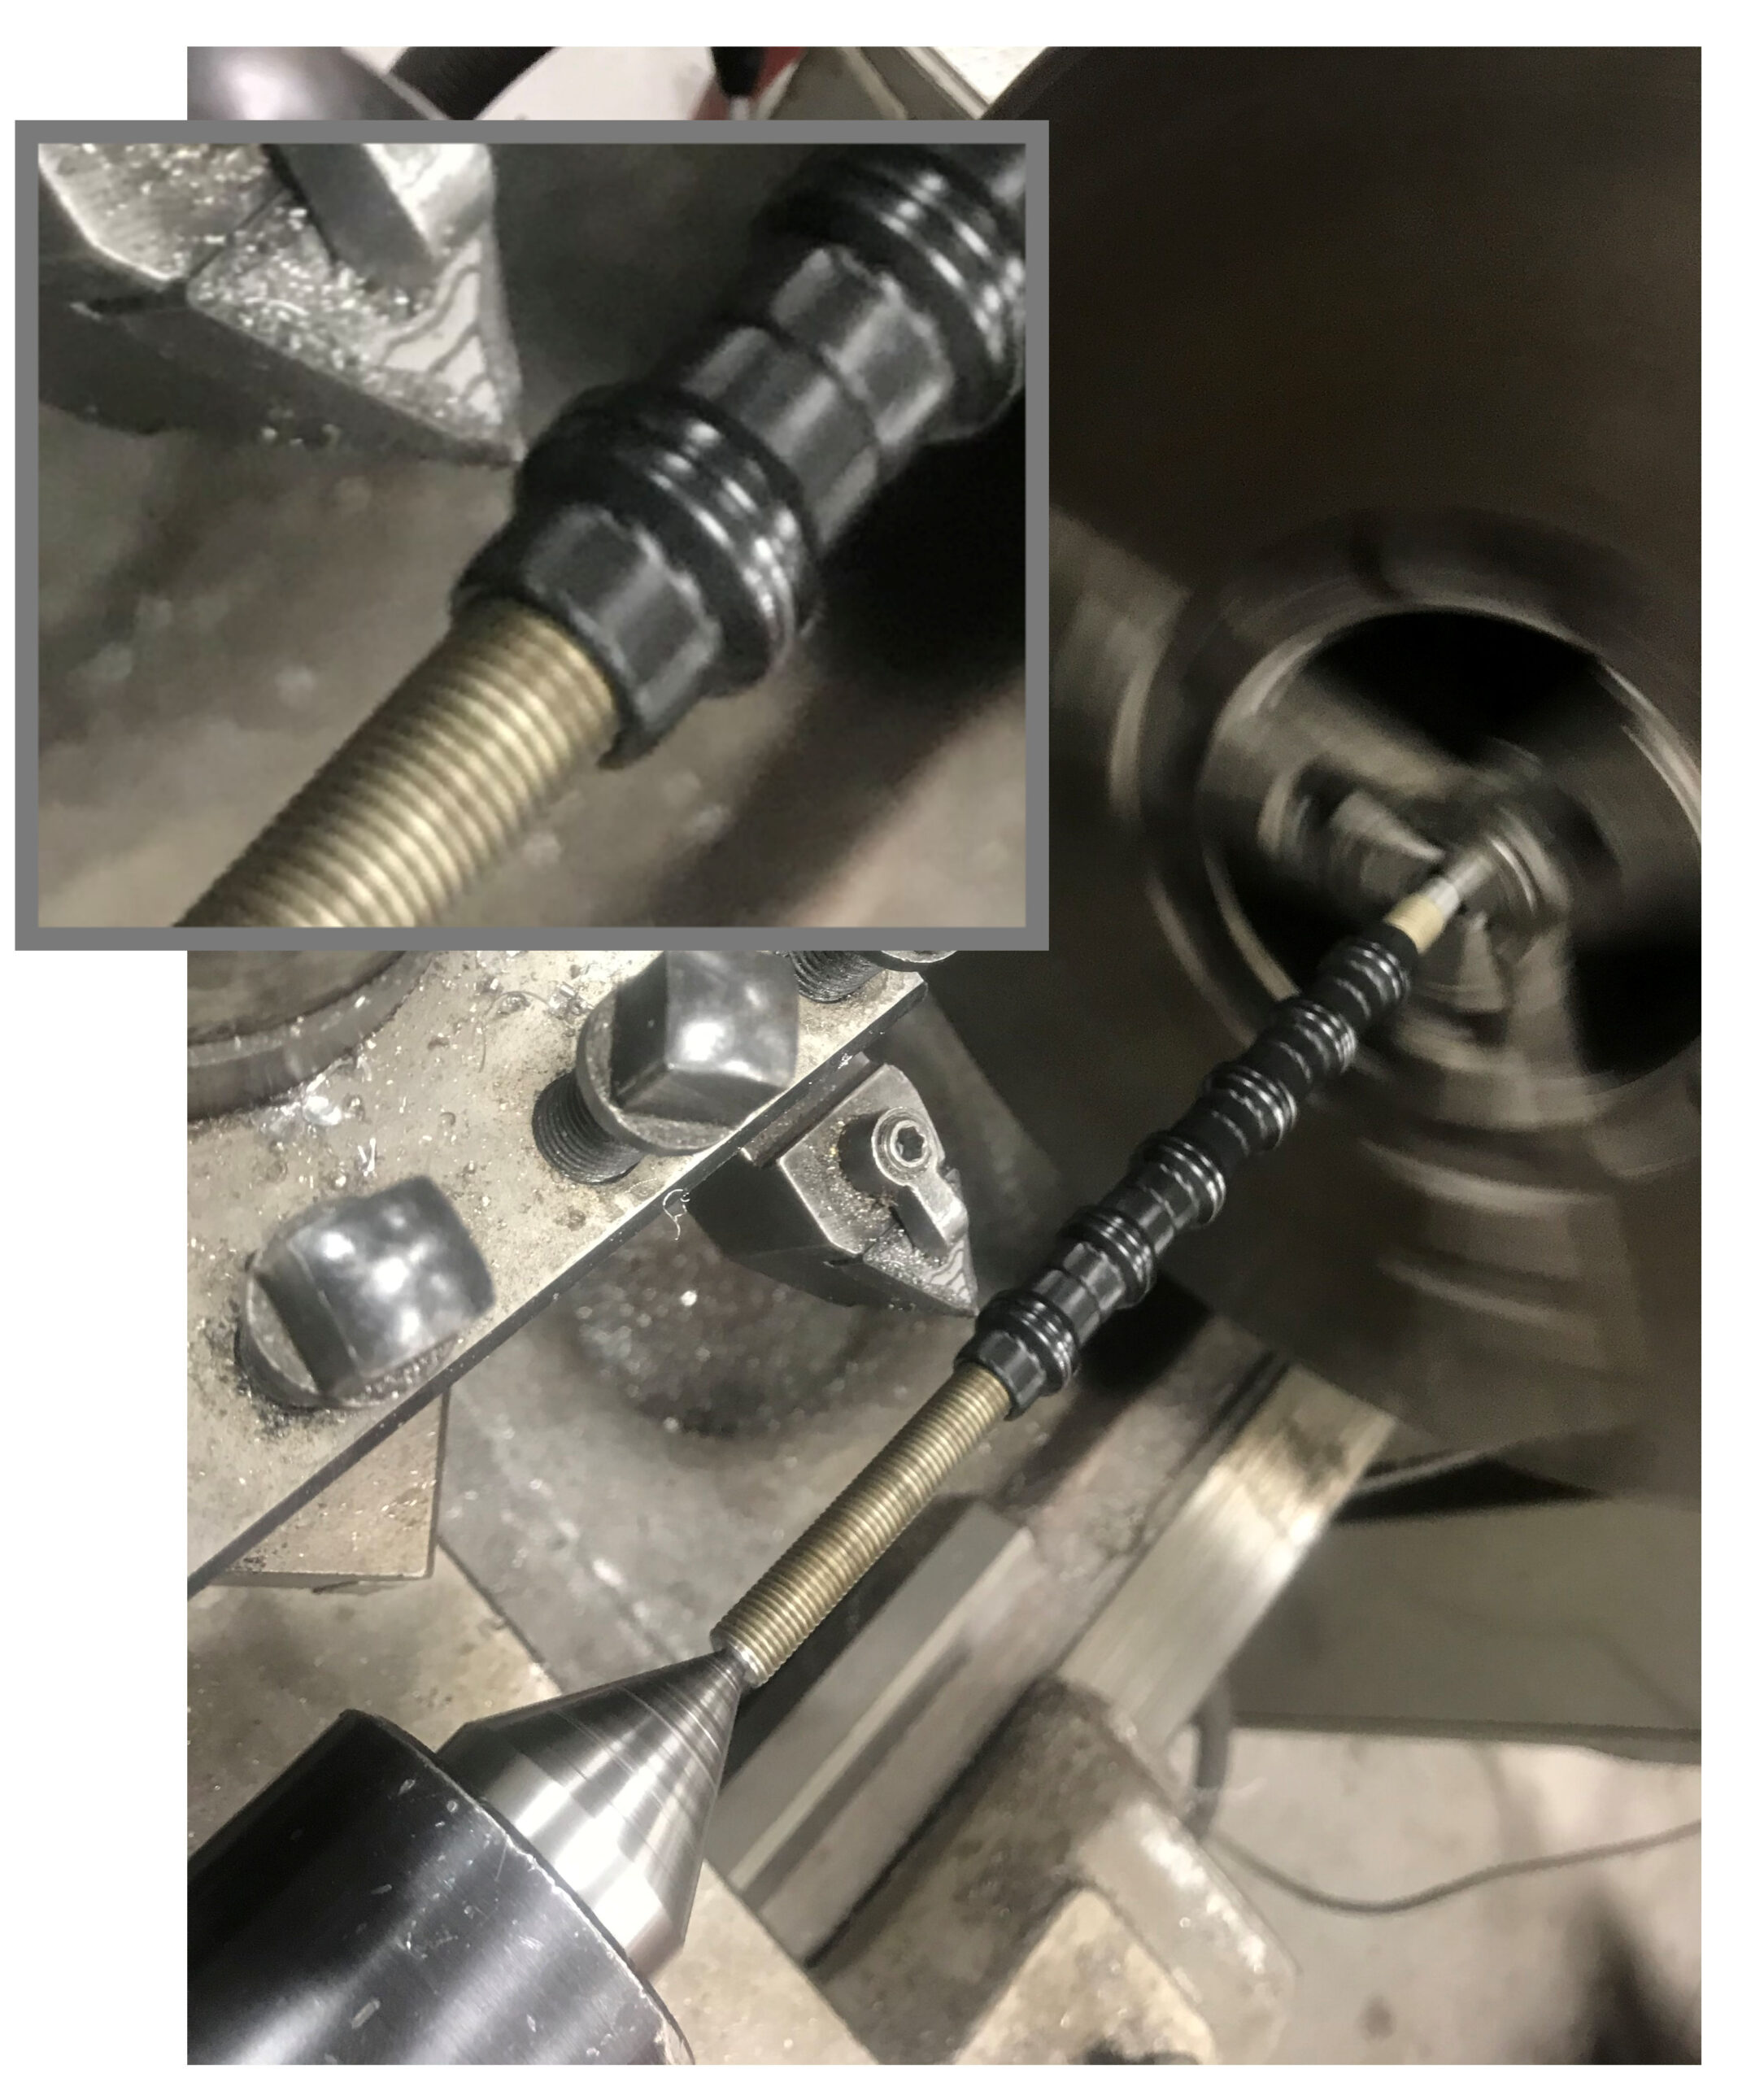
ANOTHER ARBOR To cut down the flange on 12-point nuts for clearance, we built this simple arbor which allows us to cut 12 at a time. Simply a piece of all-thread cut on one end to clamp in the jaws and drilled for a pilot hole on the other for the lathe tail stock....
GIVE IT SOME BODY
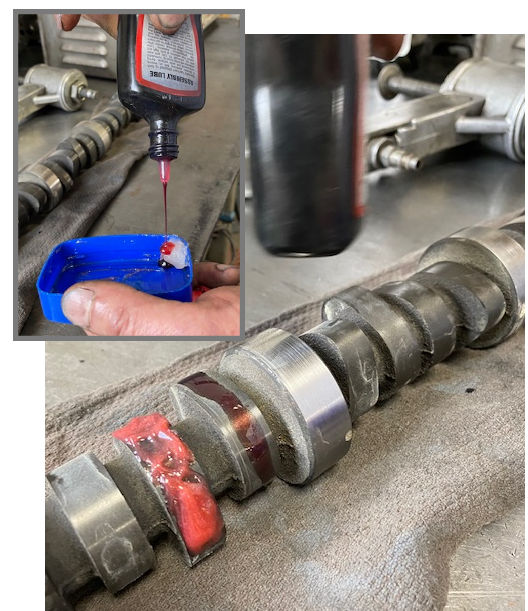
GIVE IT SOME BODY Some cam lubes are thin and drip off the cam lobes. I take thin lube and add gel capabilities to hold on to the cam lobe until start up. To do this, I add a small amount of petroleum jelly to thin cam lubes. It gives them more body so they’ll stay in...
SLEEVE LOCKS
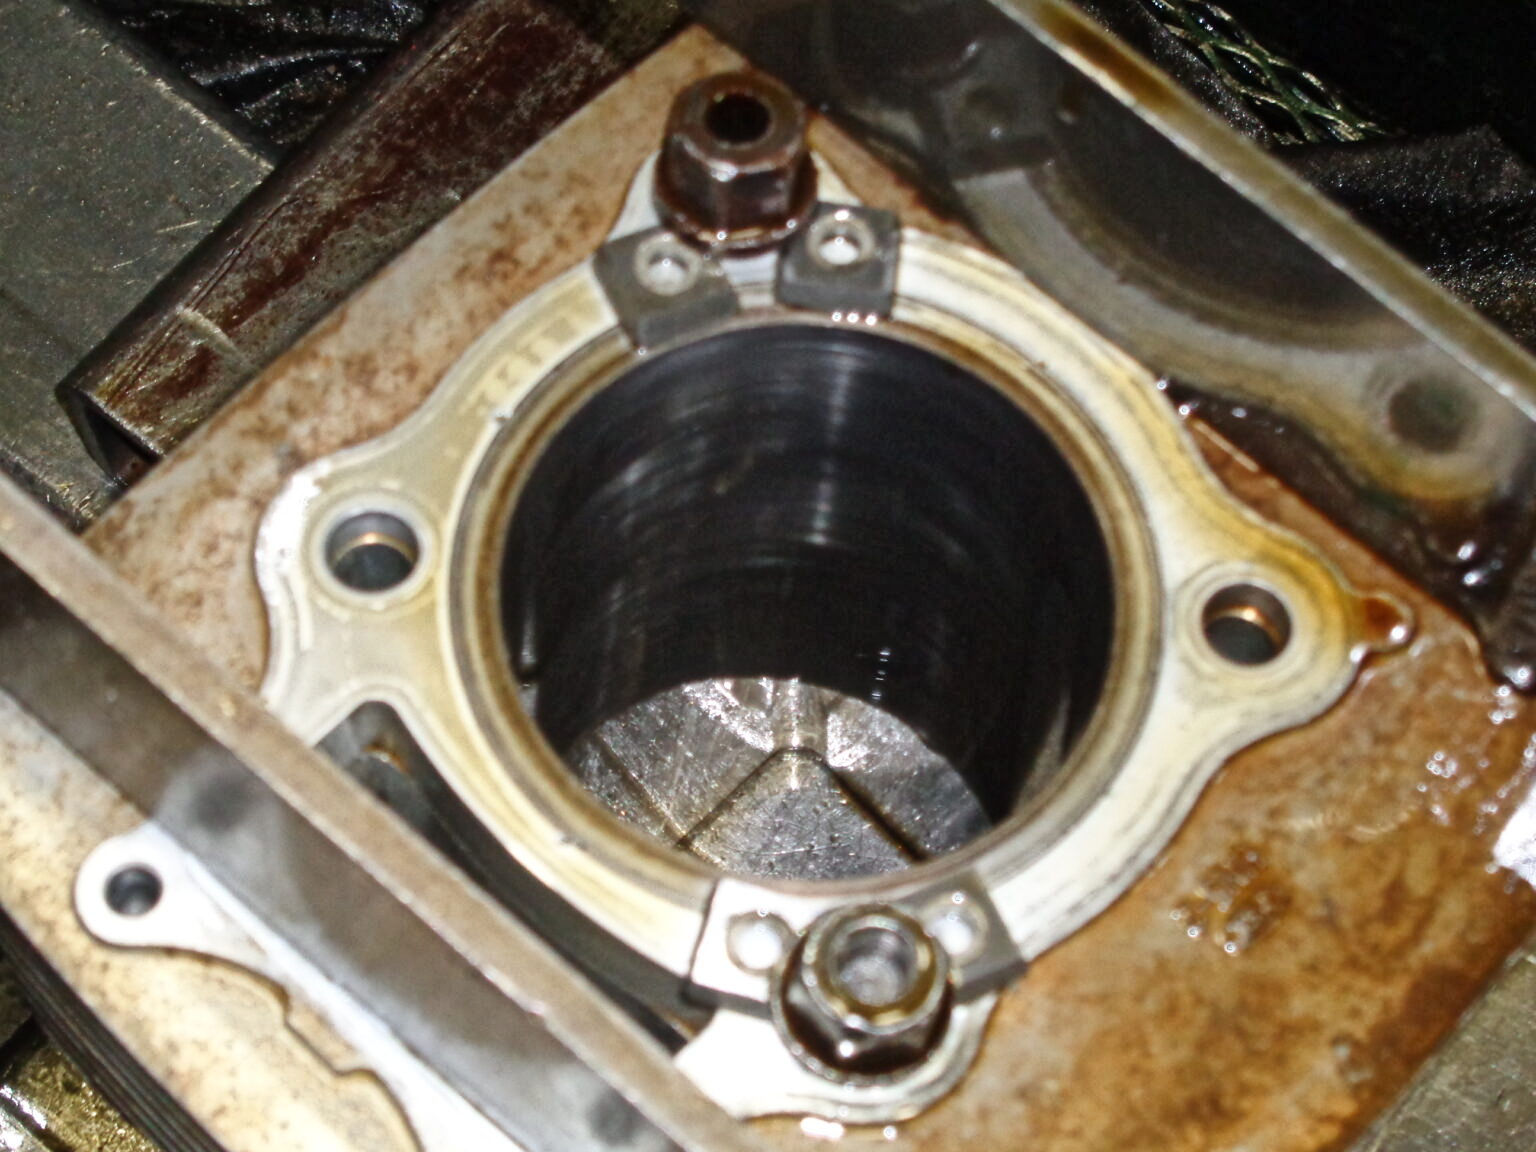
SLEEVE LOCKS When boring and honing engines with sleeves that have only a light press fit, we have found that the torque from the honing operation may cause the sleeve to slip in the engine case. We use 4 old 4-sided carbide inserts and some clamp bolts and nuts from...
REPEATABILITY KEY TO PROFITABILITY
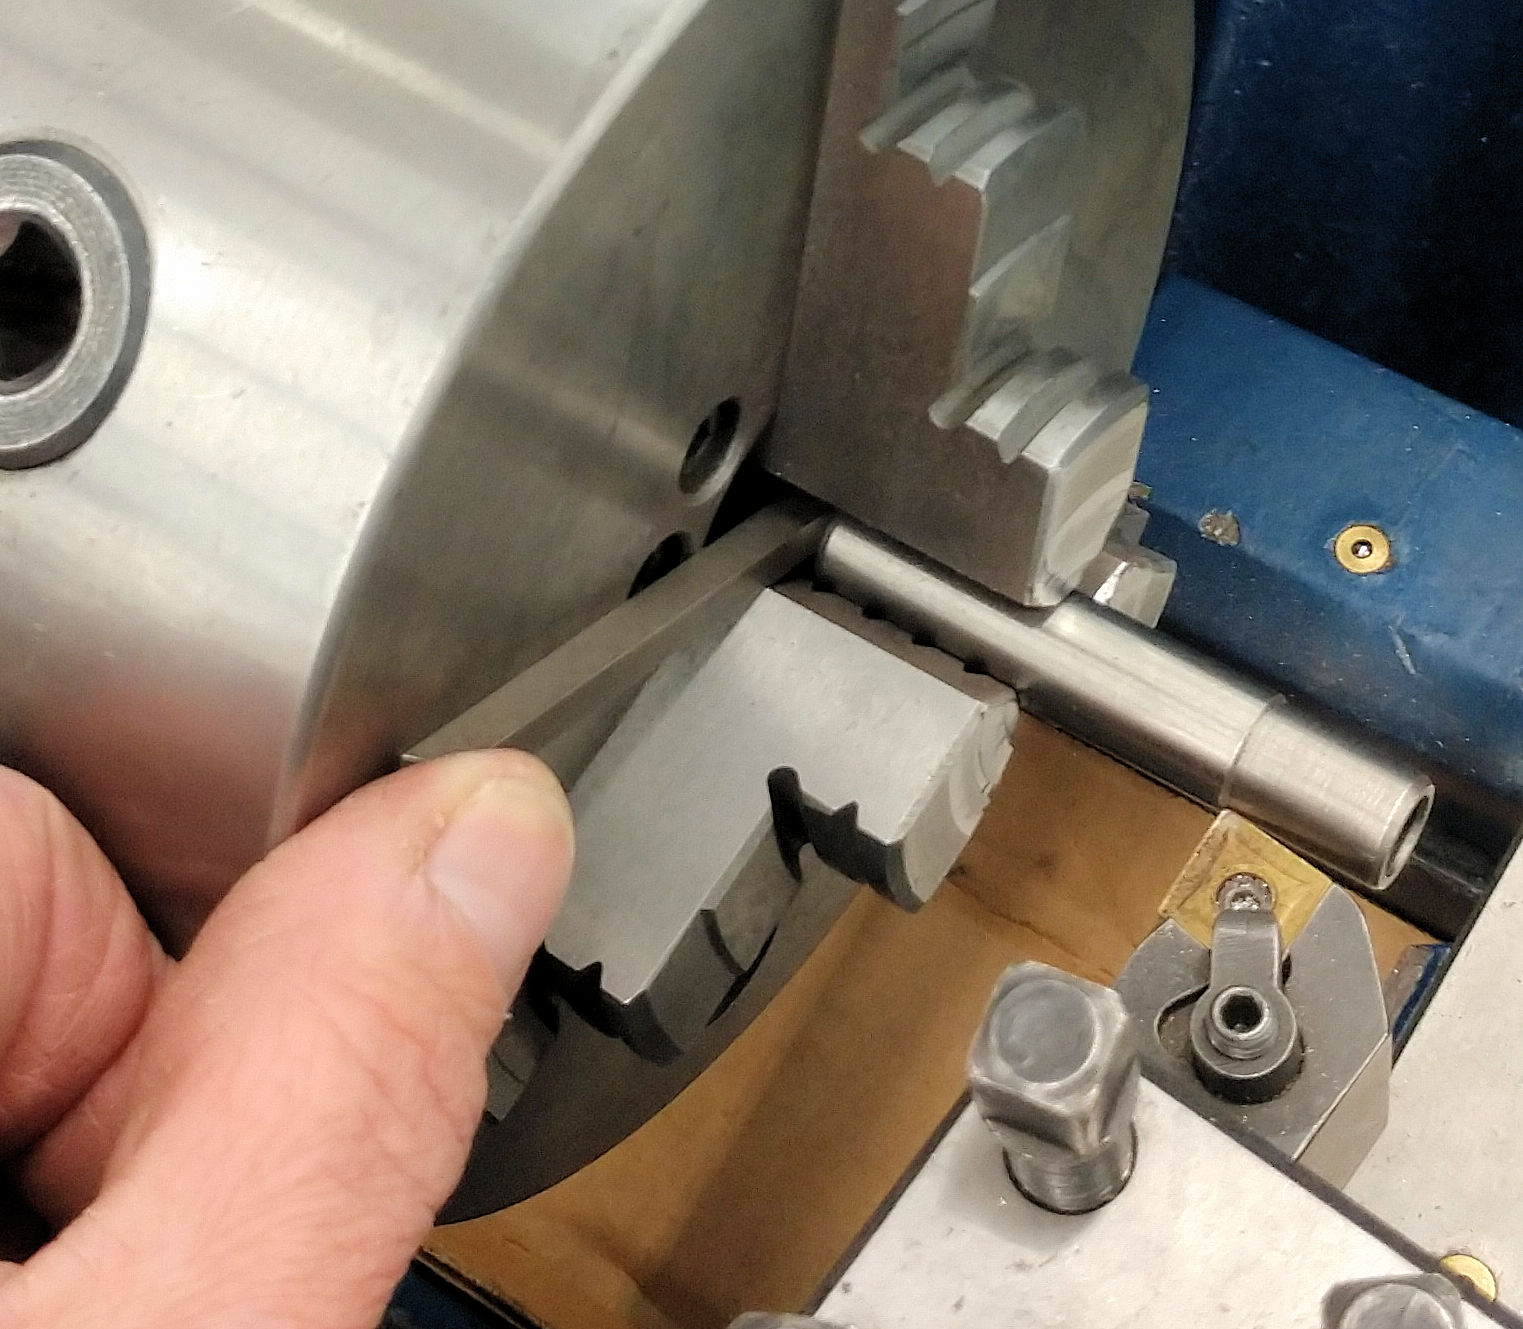
REPEATABILITY KEY TO PROFITABILITY When machining multiple parts, put your first part up against a stop like this small parallel. Machine your first one then set and zero the indicator. Now just chuck up the next part the same way. Now you do not have to measure each...