by Donnie Hurt | Oct 19, 2026 | CAMSHAFTS & VALVE TRAIN
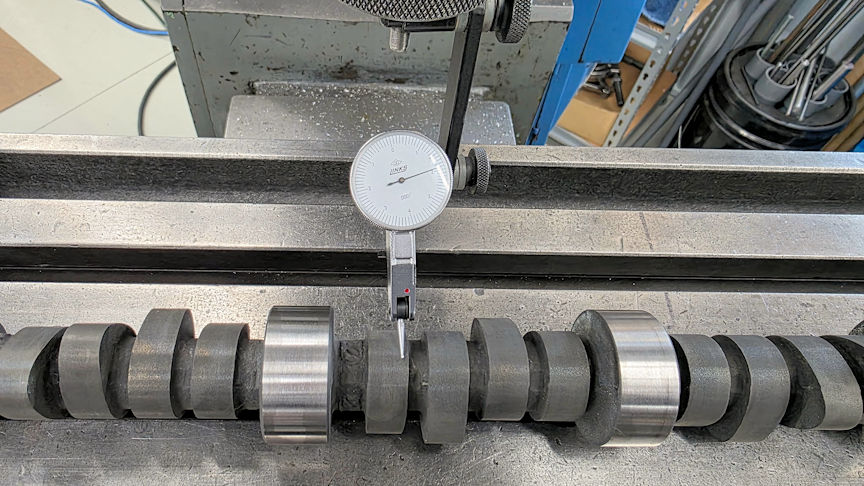
I always check the lobe taper on new flat-tappet camshafts to make sure they have adequate taper, as I prefer. Chevys are easy because the journals are all the same diameter. I lay them on the mill table and use a tenth indicator with a stem that fits in a collet. I...
by Donnie Hurt | Oct 8, 2026 | OPERATIONS
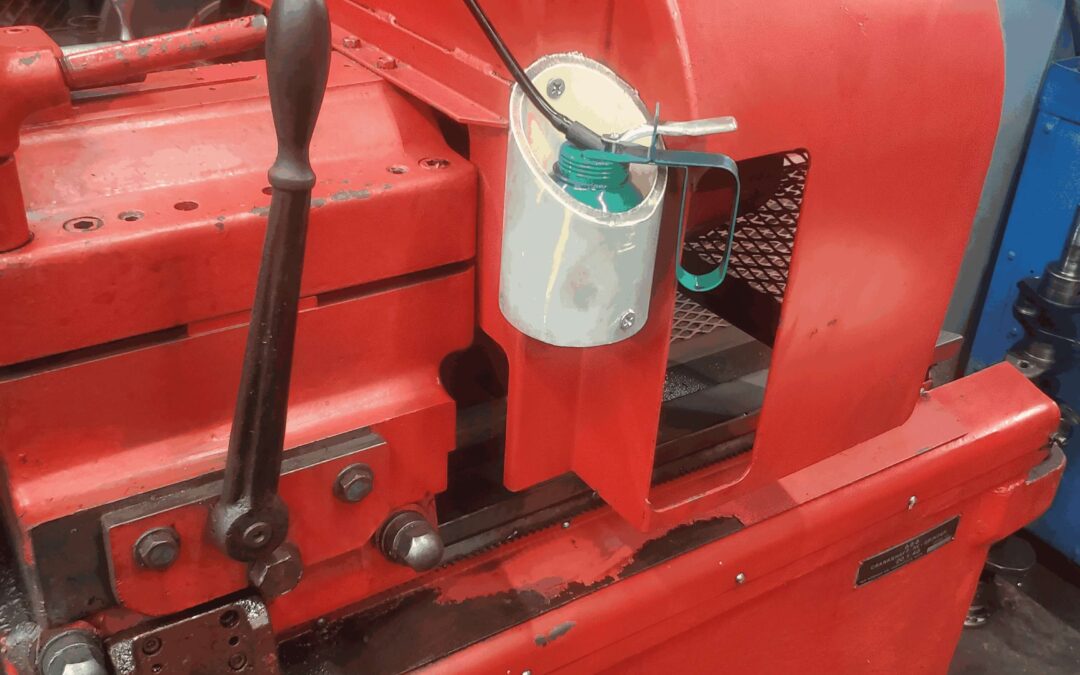
I find that in places of the shop where I’m constantly using either brake cleaner or pump oil cans that a piece of 3″ PVC, cut at a 45-degree angle, attaches very easily to a machine with one screw. For aerosol cans a few screws in the bottom will keep the...
by Donnie Hurt | Sep 28, 2026 | BLOCK WORK
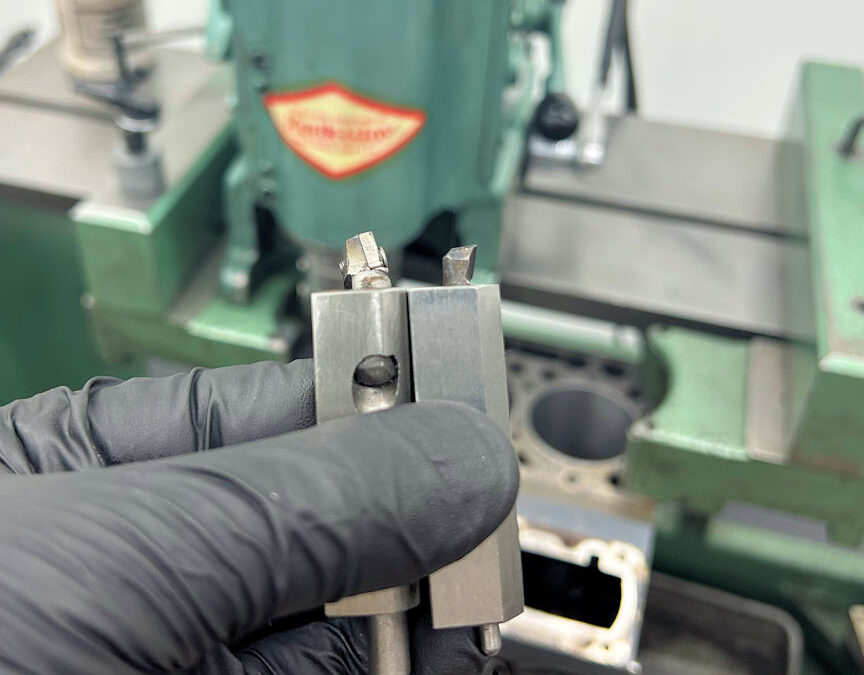
When you use different bit styles on boring bars, the size they cut can vary widely, depending on where the cutting tip is tangent to the bar centerline. Checking my own, I found there was a .007″ difference between standard-type bits and the indexable...
by Donnie Hurt | Sep 21, 2026 | DISASSEMBLY & CLEANING
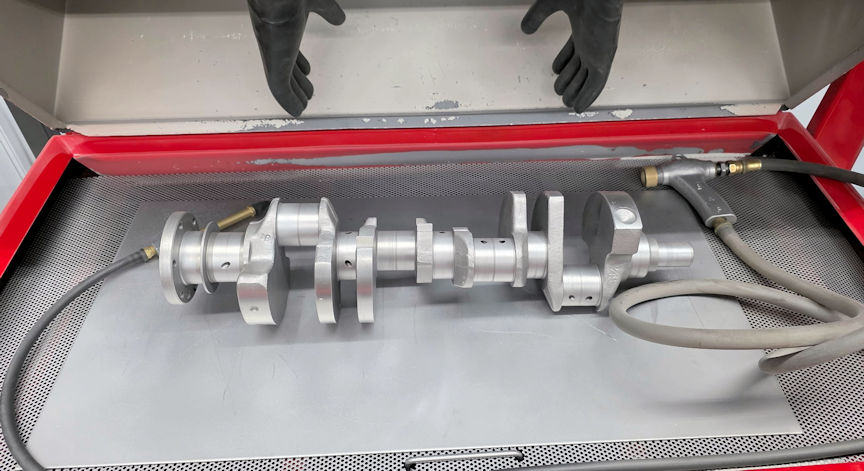
I always put a sheet of 10-gauge sheet metal in the blaster. It makes the heads and heavier parts easier to slide around. It also wears instead of the screen. Randy Torvinen Torvinen Machine Menahga, MN
by Donnie Hurt | Sep 14, 2026 | CRANKSHAFTS & CONNECTING RODS
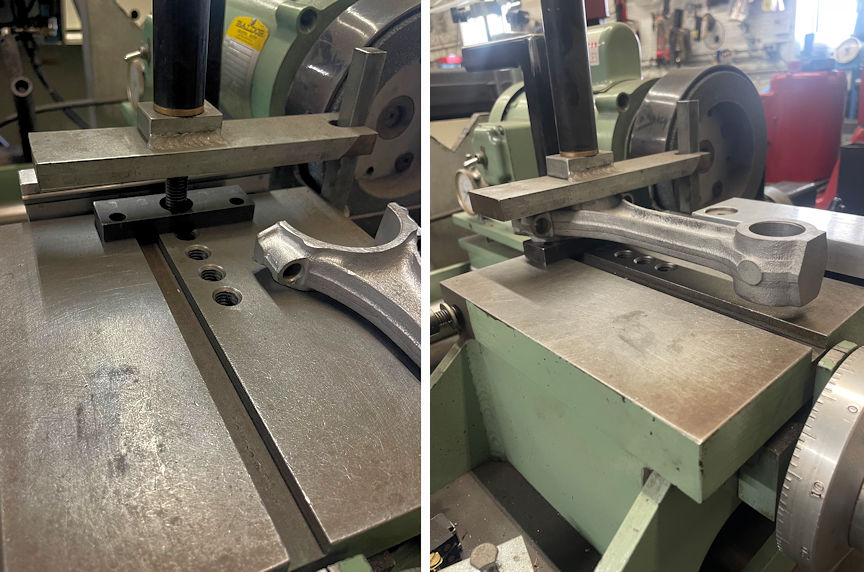
When I resize Pontiac rods where the pin boss is wider than the big end, I need to lift the rod up to use the Delta Grinder. I use a spacer from my CK10 to make the job simple. Dwayne Corrigan DC Machine Performance Engines Foley, MN